

8 Jun 2026
Changeover Optimization: Why White After Black Takes Three Times Longer
The same three jobs can cost 35 or 80 minutes of changeover, depending only on their order. Learn setup matrices, SMED and when longer campaigns stop paying.
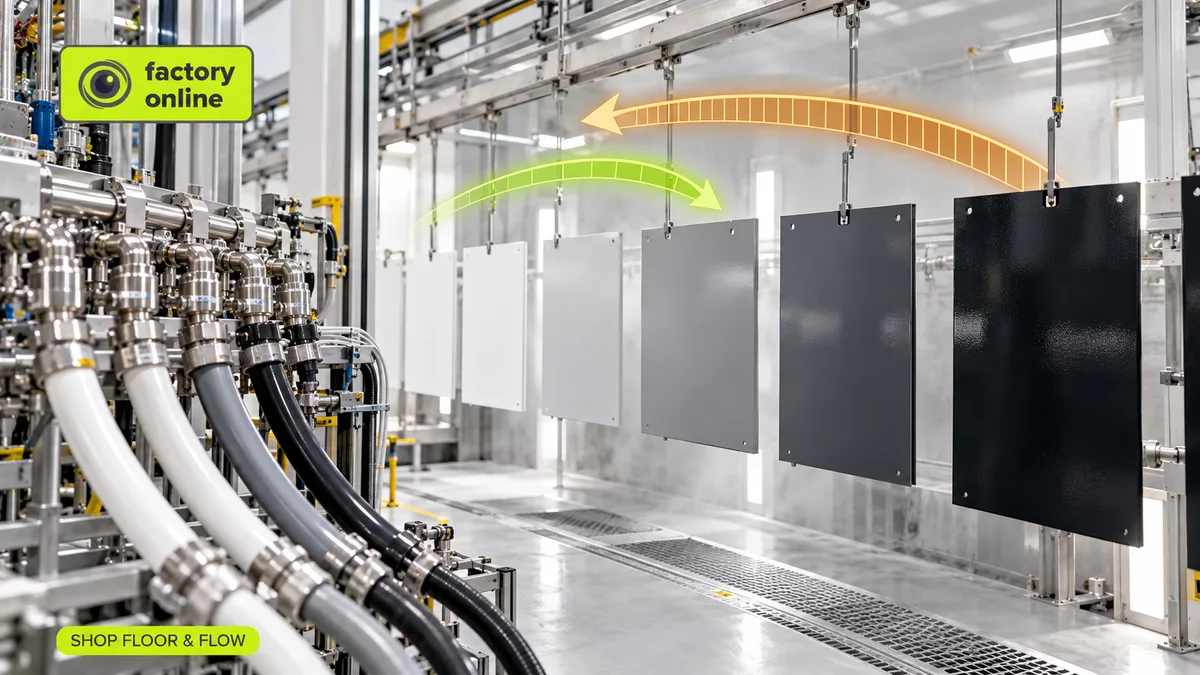
On a paint line, switching from white to black takes 20 minutes: flush the lines, a little purge, done. Going the other way, from black to white, takes 60. Every trace of black pigment has to leave the pumps, hoses and guns, or the next thousand white parts come out gray. Same two colors, same line, and white after black takes three times longer than black after white.
That asymmetry is the whole idea behind changeover optimization: arranging the order of jobs and the way setups are done so a machine spends as little time as possible switching between products. The number of changeovers matters less than which ones you pick.
Setup time belongs to the pair, not the product
Most ERP systems store one setup time per product. "White: 30 minutes." But a setup is a trip from one product to another, and the length of the trip depends on where you start. Planners call this a sequence-dependent setup. The honest way to write it down is a from-to matrix.
Here is one for three colors (minutes):
- White → Gray: 15, White → Black: 20
- Gray → White: 30, Gray → Black: 20
- Black → White: 60, Black → Gray: 40
Now schedule the same three jobs two ways, starting from a clean line.
Black, Gray, White: 40 + 30 = 70 minutes of changeover.
White, Gray, Black: 15 + 20 = 35 minutes.
Same jobs, same line, half the lost time. And if you sort strictly by due date and it happens to give you Gray, Black, White, you pay 20 + 60 = 80 minutes. That is why production scheduling by due date alone so often produces a late schedule.
The light-to-dark wheel in cable plants
Cable plants live with this every day. On an extrusion line, the insulation or jacket compound changes color, and a light color after a dark one means purging until the melt runs clean. Every meter of purge is scrap. So extrusion is usually planned as a wheel: natural, then white, yellow, red, blue, black, and a full clean before the wheel starts again. Die and tip changes for a different cross-section are a second layer of the same matrix. Getting both layers right on the busiest line is a big part of cable manufacturing planning.
SMED: the Formula 1 pit stop
Sequencing picks the cheapest changeovers. SMED makes each changeover cheaper. The method comes from Shigeo Shingo's work at Toyota; the name stands for Single-Minute Exchange of Die, meaning a changeover under ten minutes.
The best analogy is a Formula 1 pit stop. Four wheels change in under three seconds, and not because the mechanics are fast with a wrench. Everything that can happen while the car is still on track already has: tires warmed and waiting, crew in position, tools in hand. The car stops only for work that truly needs it stopped.
SMED splits a changeover the same way:
- Internal work needs the machine stopped: swapping the die, cleaning the head.
- External work can happen while the previous job still runs: fetching the next die, staging material, printing labels, preheating.
A typical first study finds a 60-minute changeover where 25 minutes are external work done at the wrong time. Move it before the stop and the changeover drops to 35 minutes without buying anything.
Myth: longer campaigns are always cheaper
Grouping jobs into long campaigns cuts changeovers, but every campaign builds stock. Say a line sells 500 white parts a week. Run white once a week and you make 500 at a time, so average stock is about 250. Run it every two weeks and you make 1,000 at a time; average stock doubles to about 500. You save one changeover every two weeks and pay for it with 250 extra parts sitting on the shelf, plus the risk that the customer changes the spec.
Whether that trade is worth it depends on one question: is this machine the bottleneck? An hour saved on the constraint is an hour of extra output for the whole plant. An hour saved on a machine that already waits for work is worth almost nothing. Manufacturing optimization explains how to find that machine. On the bottleneck, changeover loss is also one of the biggest hidden pieces of OEE.
How to start
- Pick the line where changeovers hurt most and write its from-to matrix with operators, not from the ERP.
- Agree when a changeover ends: first part started, or first good part. Trial runs count.
- Film one changeover and mark every step internal or external.
- Set a sequence rule (light to dark, small to large die) and let due dates override it only when a late order is the real cost.
How it looks in factory.online
In factory.online, the planner sees the extrusion line's jobs on a finite-capacity Gantt and can save the due-date order and the light-to-dark order as two planning scenarios. Side by side, the question gets concrete: which orders finish late in each version, and how many hours the line gives back. Purge scrap reported in output and scrap confirmations shows what each color switch really cost.
BEEDIGIT collects machine and operator data for OEE, downtime and actual production reporting. These records help the team compare planned capacity with what the equipment actually achieved and investigate recurring losses.
If one of your lines loses a shift a week to color changes, book a demo and we'll look at its sequence together.
