

13 Jul 2026
Supply Chain Management: The Bullwhip Effect Inside Your Factory
Customers bought 10% more and your supplier saw an 80% jump. Learn how the bullwhip effect works, what a volume discount really costs, and why department KPIs pull apart.
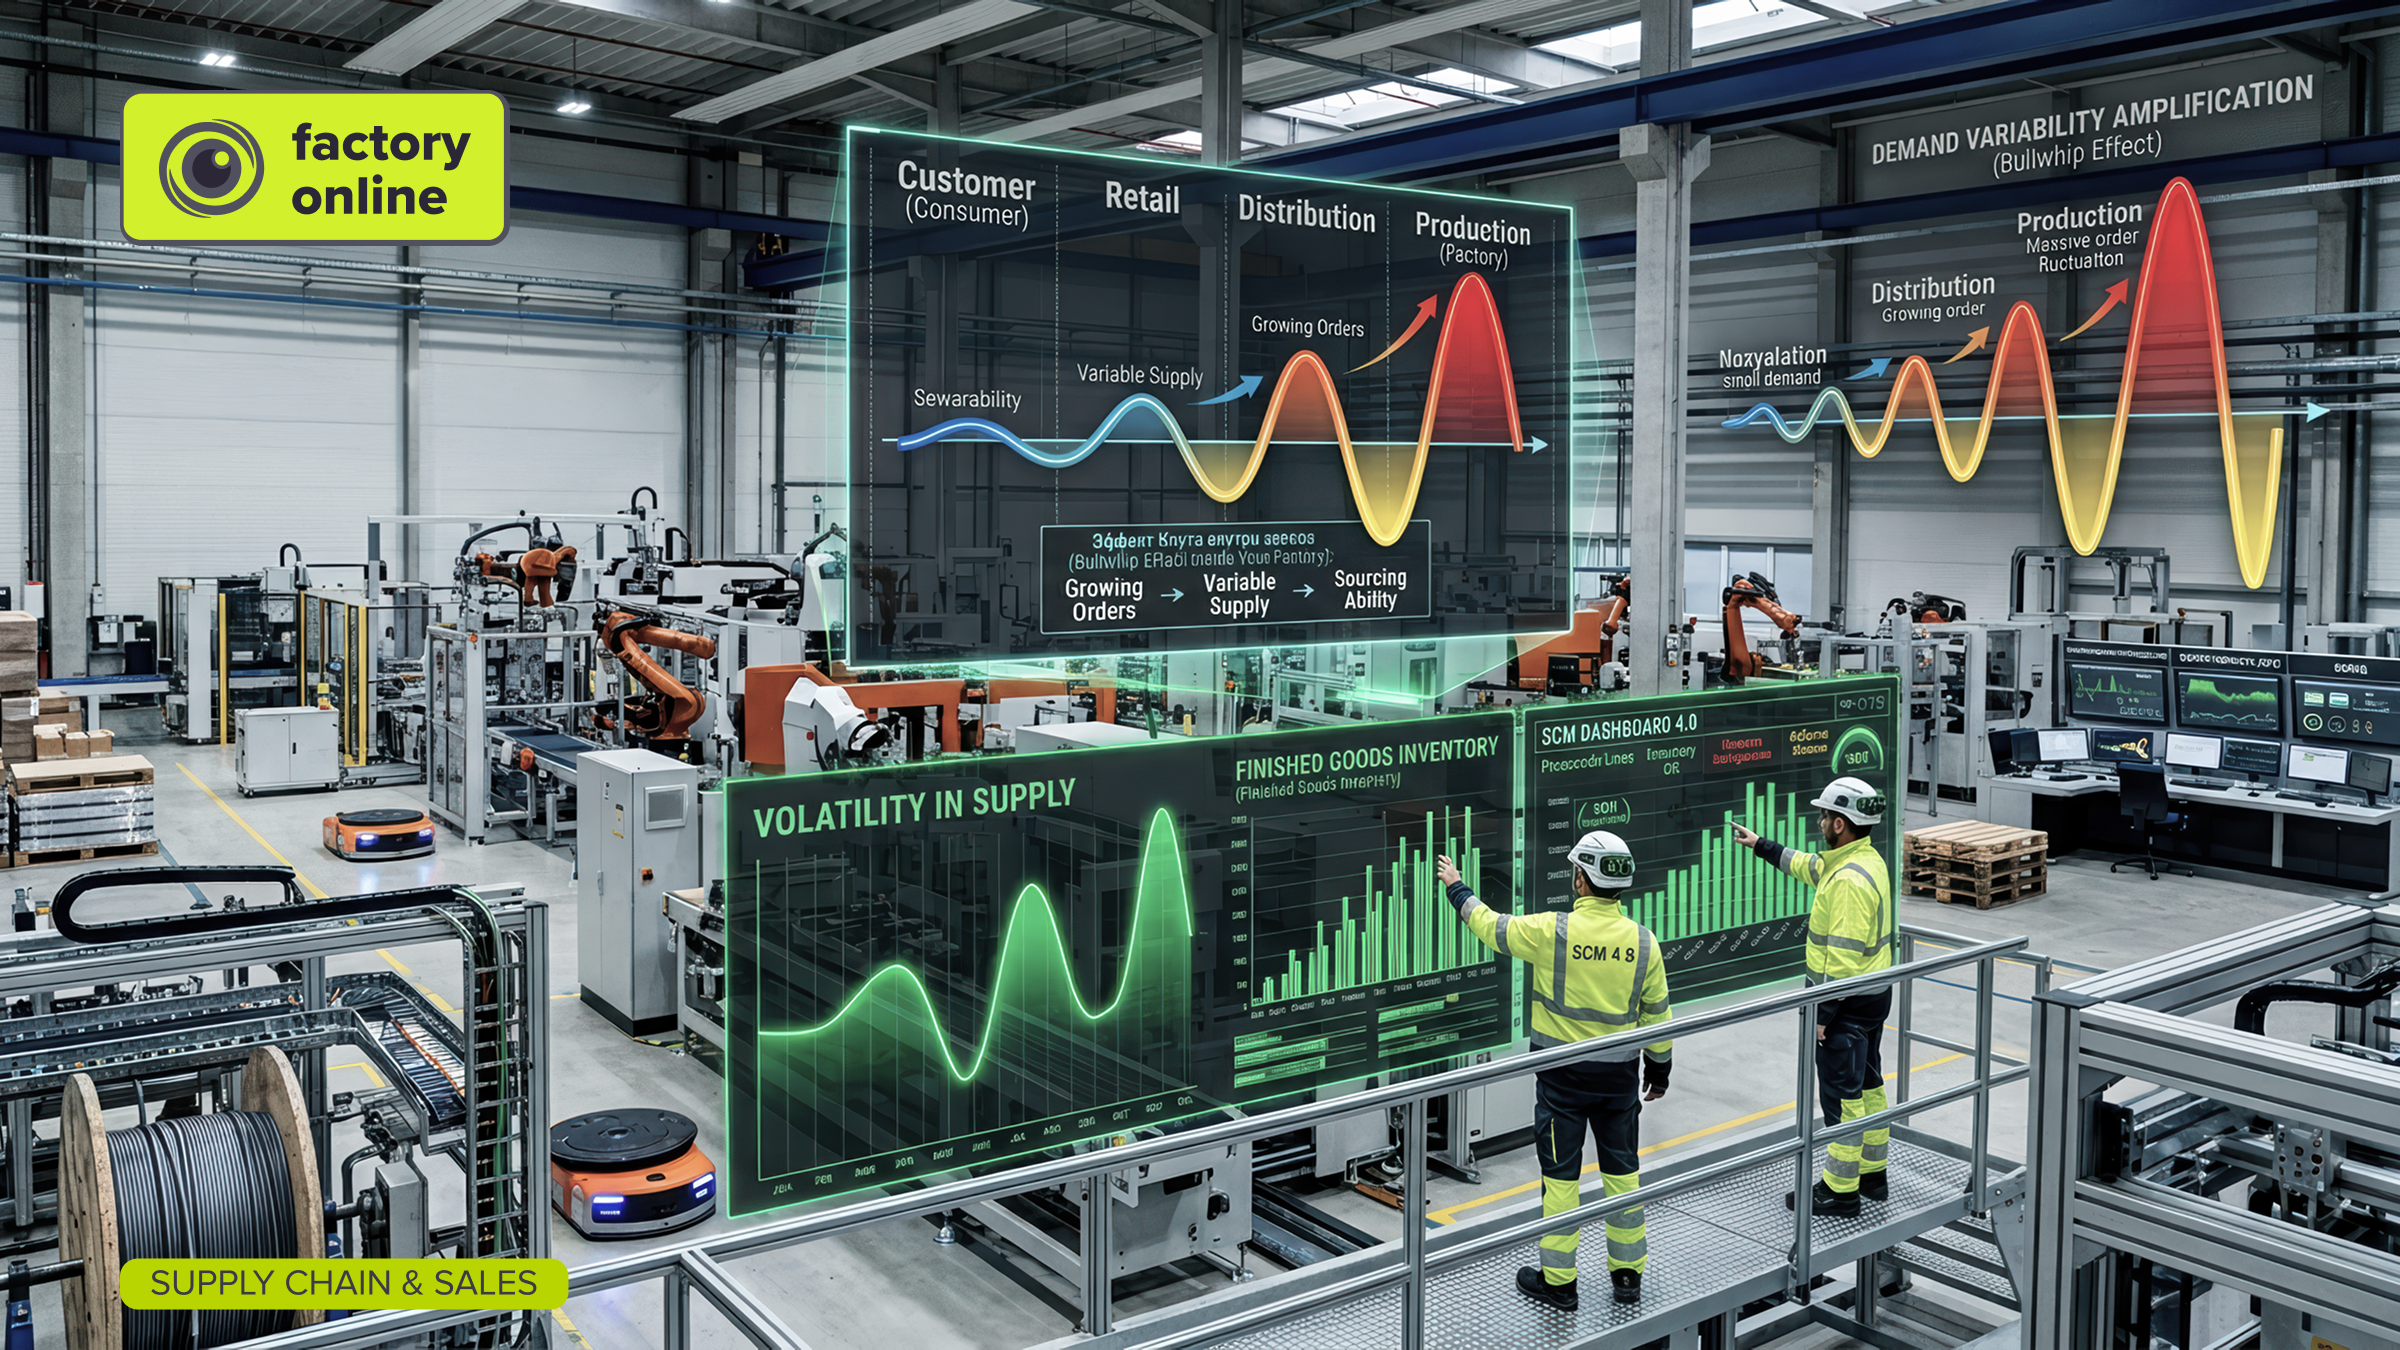
A retailer's customers buy 10% more of your product. Nothing dramatic: a warm week, a small promotion. That same week your raw material supplier sees an order 80% larger than usual. The week after, your order drops to 60% of normal. The supplier concludes you have no idea what you are doing. From your seat, every step looked reasonable.
This is the bullwhip effect, and it is the best place to start understanding supply chain management: the coordination of purchasing, production, inventory and distribution so that materials and products flow from suppliers to customers at the lowest total cost and with reliable delivery. The key word is total. Most supply chain problems come from each link doing its own job well.
What the bullwhip effect is
The bullwhip effect is the way small changes in customer demand grow into large swings in orders as they move up the supply chain. Crack a whip with a small flick of the wrist and the tip moves several feet.
The classic demonstration is the "beer game," developed at MIT in the 1960s. Four players run a retailer, a wholesaler, a distributor and a brewery, each seeing only the next player's orders. Customer demand changes once, by a small step, and within a few rounds most teams swing between empty shelves and overflowing warehouses. Nobody made a crazy decision. The structure did it.
The bullwhip effect in numbers
Here is an illustrative example with four tiers: retailer, distributor, your factory, your supplier. Each tier follows one sensible rule: order what you just sold, plus enough to keep one week of stock at the new sales rate. Normal demand is 100 units a week, and every tier holds 100 in stock.
Week 1: the customer buys 110 (+10%).
- Retailer sold 110. New stock target is 110, up 10. Order: 110 + 10 \= 120.
- Distributor sees an order of 120. New target 120, up 20. Order: 120 + 20 \= 140.
- Your factory sees 140. New target 140, up 40. Order to supplier: 140 + 40 \= 180.
The supplier sees +80%. Each tier doubled the change.
Week 2: the customer keeps buying 110. Demand is stable now.
- Retailer sold 110, target unchanged. Order: 110.
- Distributor sees 110. Target drops from 120 to 110. Order: 110 − 10 \= 100.
- Your factory sees 100. Target drops from 140 to 100. Order: 100 − 40 \= 60.
Customer demand: 100, 110, 110. Supplier orders: 100, 180, 60. Add real lead times, batch sizes and a sales team that "orders a bit extra just in case," and the swings get worse.
The bullwhip inside your own factory
You don't need four companies for this. Sales, planning, production and purchasing are tiers too:
- Sales pads the forecast by 10% "to be safe."
- Planning rounds the production order up to a full batch.
- Purchasing rounds the material order up to a truckload, then adds safety stock.
Three reasonable decisions, and a 10% demand change can easily become a 40% jump in material orders. When the extra stock arrives and demand has not moved, purchasing cuts the next order hard. The supplier sees a whip.
The fix is the same inside and outside the walls: share the real demand signal, not just the order you derived from it. That is the purpose of a monthly S\&OP process where sales, operations and finance look at one set of numbers. Other remedies from the research: shorter lead times, smaller and more frequent orders, and stable pricing that doesn't reward customers for buying in waves.
Think of a shower with a slow hot water pipe. You turn the tap, nothing happens, you turn it more, and ten seconds later you are scalded. Delay plus reaction equals overshoot.
Total cost: when the 5% discount loses money
The second supply chain lesson is about cost. A supplier offers 5% off if you buy six months of a part at once instead of monthly.
The numbers: you use 1,000 units a month at $100.
- Monthly buying: average stock is half a month, 500 units, worth $50,000.
- Six-month lot at $95: 6,000 units. Average stock is 3,000 units, worth $285,000.
The discount saves 6,000 × $5 \= $30,000. But you now carry $235,000 more inventory on average for six months. At a carrying cost of 2% per month (24% a year, a common planning assumption covering capital, space, insurance and obsolescence), that costs $235,000 × 2% × 6 \= $28,200.
Net saving: $1,800. One engineering change that makes the part obsolete, or one month of rented overflow space, wipes it out. Rule of thumb: if the extra stock waits roughly three months longer than it would have, carrying cost eats a 5% discount. Before accepting the deal, check the other options for the same money; six shortages that don't need a new purchase order is a good list.
Myth: "Each department hitting its KPI means the chain works"
Every department in this article did its job:
- Purchasing hit its price-variance target with the 5% discount.
- Production hit its OEE target by running long batches.
- Sales hit its fill rate by padding the forecast.
The company paid for all three: more stock, more swings, and late orders for products that were not in the long batch. Local KPIs are useful, but only in pairs that pull against each other: price variance with inventory days, OEE with on-time delivery, forecast accuracy with forecast bias. How to build those pairs is covered in manufacturing KPIs.
The same goes for where finished stock sits: stock in the wrong warehouse fails customers like no stock at all, as distribution planning shows.
What good supply chain management looks like in a plant
- One demand signal. Customer orders and one agreed forecast, visible to planning and purchasing without anyone adding a private buffer.
- Orders linked to their reason. A purchase need that can be traced to the customer orders behind it is much harder to inflate.
- Total cost decisions. Price, carrying cost and risk on the same page before a big buy.
- Short, reliable lead times. A shorter pipe means less overshoot.
FAQ
What causes the bullwhip effect? Mainly delays, order batching, forecasting from the next tier's orders instead of end demand, and price promotions. Customer demand is often steadier than it looks from the factory.
Is supply chain management the same as logistics? No. Logistics moves and stores goods. Supply chain management also decides what to buy and make, and when.
How it looks in factory.online
In factory.online, sales orders create manufacturing demand, and MRP runs through multi-level BOMs, stock and open supply with every shortage linked to the order that created it. When the factory's material requirement jumps from 100 to 180, the planner can open it and see which customer orders are behind it, and whether the jump is new demand or just a stock target moving. Planning scenarios let you compare a padded plan with the actual order book before a purchase order goes out.
If your suppliers see more drama than your customers create, book a demo and bring the last swing with you.
