17 Sep 2026
Production Scheduling Software for Small Manufacturers: What Actually Matters
Enterprise APS vendors sell features you will never switch on. Here is the short list of capabilities a 20–200 person plant genuinely needs from scheduling software — and what to ignore.
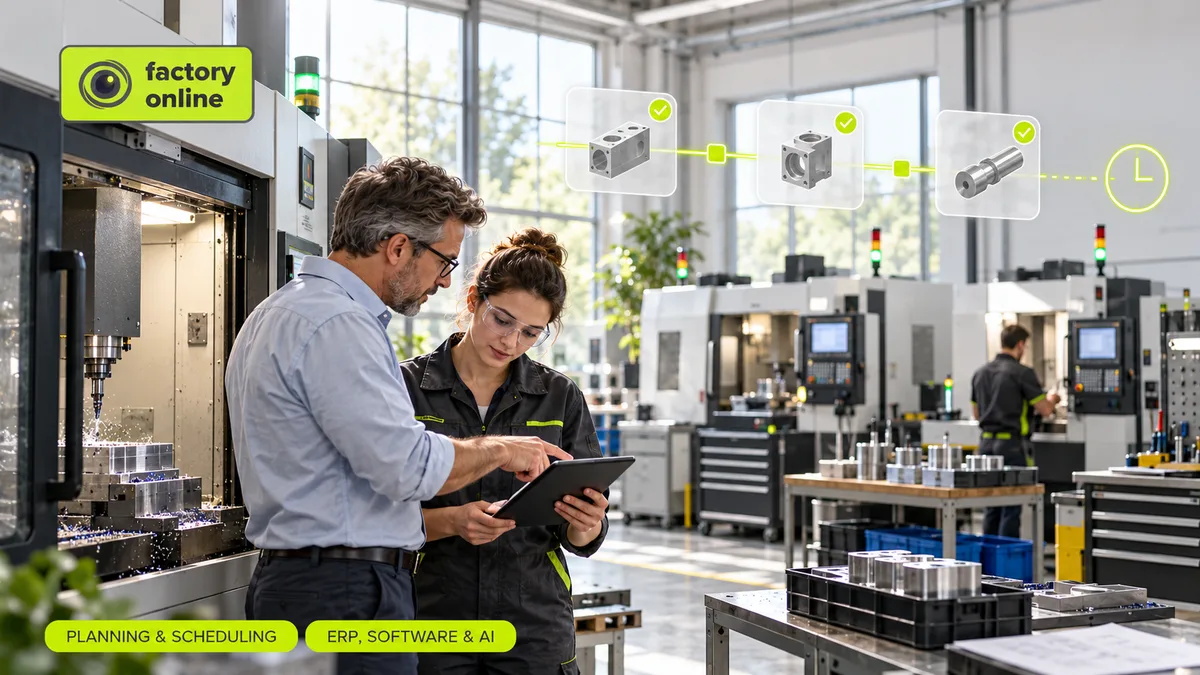
Search for production scheduling software and you will land on demos built for aerospace corporations: eighteen-month implementations, a dedicated planning department, a six-figure budget. If you run a plant with 20 to 200 people, most of that is noise.
Here is what actually matters when a small manufacturer chooses scheduling software — distilled from how these plants really work.
1. Finite capacity, not infinite to-do lists
The single feature that separates scheduling software from a task list: the system knows a work centre can only run one job at a time, for the hours it is actually staffed. If a tool lets you stack three jobs on the same machine at 10:00, it is a calendar, not a scheduler.
2. Replanning speed
Your schedule will break today. The only question is how long the fix takes. In a small plant there is no planning department to rebuild the week — the owner or production manager does it between other jobs. Look for automatic rescheduling: a breakdown or rush order should resequence affected jobs in seconds, not in an evening of drag-and-drop.
3. Data you already have
Enterprise systems assume pristine master data maintained by specialists. Small plants need software that works with what exists: orders, BOMs, routings, work centres. If the vendor's first phase is a three-month data cleansing project, walk away.
4. The shop floor actually uses it
A schedule that lives in the office is half a solution. Operators need to see today's sequence per work centre and report progress without a training course. If the demo requires a manual for the shop floor view, adoption will fail.
5. Alternatives and changeovers
Small plants survive on flexibility: the same part runs on two machines, setups eat hours. The scheduler should know alternative work centres and changeover times between products — this is where the hidden capacity sits.
What to ignore
- Optimization algorithms you cannot explain to your own team
- Modules for industries you are not in
- Dashboards that require a data analyst to maintain
The honest test
Ask the vendor to schedule your actual next week — your real orders, your real machines, your real changeovers — during the evaluation. Software that handles your messy reality in a demo will handle it in production. Software that needs your data "prepared" first will need it forever.
We wrote about the underlying mechanics in how to plan production schedules, and about the breaking points that force replanning in what problems production scheduling solves.