10 Sep 2026
How to Plan Production Schedules Using Modern Planning Software
A practical walkthrough of building a production schedule that survives contact with the shop floor: from orders and BOMs to finite capacity, changeovers and daily replanning.
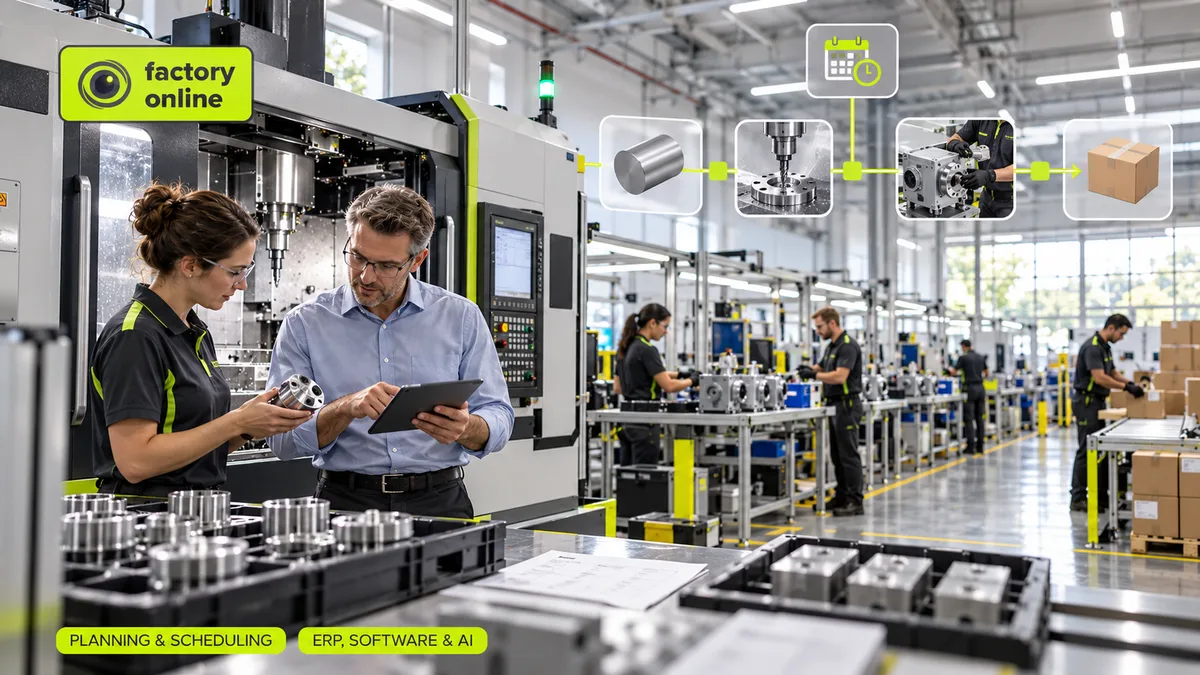
Most production schedules fail for the same reason: they are built as static pictures of a perfect day. The first breakdown, rush order or late delivery turns them into fiction, and the shop floor goes back to improvisation.
A schedule that actually works is built in a different order — from constraints outward, not from wishes inward. Here is the process we see working in small and mid-sized plants.
1. Start from confirmed demand, not from the wish list
Pull every manufacturing order that has a real due date: customer orders (MTO) and stock replenishment (MTS). Anything without a date or a quantity is not input for the schedule — it is a conversation with sales.
At this stage you should have a clean list: what, how many, by when.
2. Explode the BOM into operations
Each product becomes a chain of operations through your routing: cutting, machining, assembly, packing. Every operation carries a run time per unit, a setup time, and the work centres that can perform it — including alternatives.
If your routings live in someone's head or in a spreadsheet from 2019, this is the step where the schedule is won or lost. Inaccurate run times produce a plan that looks precise and is wrong by hours.
3. Load operations against finite capacity
This is where modern production scheduling software parts ways with the whiteboard. Each work centre has a calendar: shifts, maintenance windows, planned downtime. Operations are placed only where capacity actually exists, and alternative work centres absorb overflow automatically.
Infinite-capacity plans — the kind Excel produces — always look feasible and never are.
4. Sequence with changeovers in mind
Two identical schedules can differ by hours of lost time depending on the order of jobs. Changeover matrices — setup time from product A to product B — let the scheduler group compatible jobs and push expensive changeovers apart.
In plants with frequent product switches, sequencing alone regularly frees up a shift per week.
5. Publish one schedule the whole shift works from
A schedule nobody sees is a suggestion. The shop floor needs the current sequence per work centre, with statuses that update as jobs start and finish. When everyone looks at the same live plan, "what are we running next?" stops being a meeting.
6. Replan daily — automatically
Breakdowns, sick operators, late material: the question is not whether the plan will break, but how fast it recovers. Modern scheduling resequences affected job orders across available work centres immediately, instead of a planner rebuilding the week by hand.
If you are still rebuilding the schedule in a spreadsheet every morning, that is the signal to change tools — we compared both approaches in production schedule templates vs scheduling software.
Where to start this week
Pick one bottleneck work centre. Clean up its routing times and calendar, schedule only that centre for two weeks, and measure promise-date accuracy before and after. The delta will make the case for the rest of the plant better than any presentation.
See how factory.online builds and replans production schedules →