

30 Oct 2026
Transfer Batches: Why Should the Next Operation Wait for All 500 Parts?
The first 100 parts are ready, while the next machine waits for all 500. Compare a complete-batch transfer with a smaller transfer batch and check the real constraints.
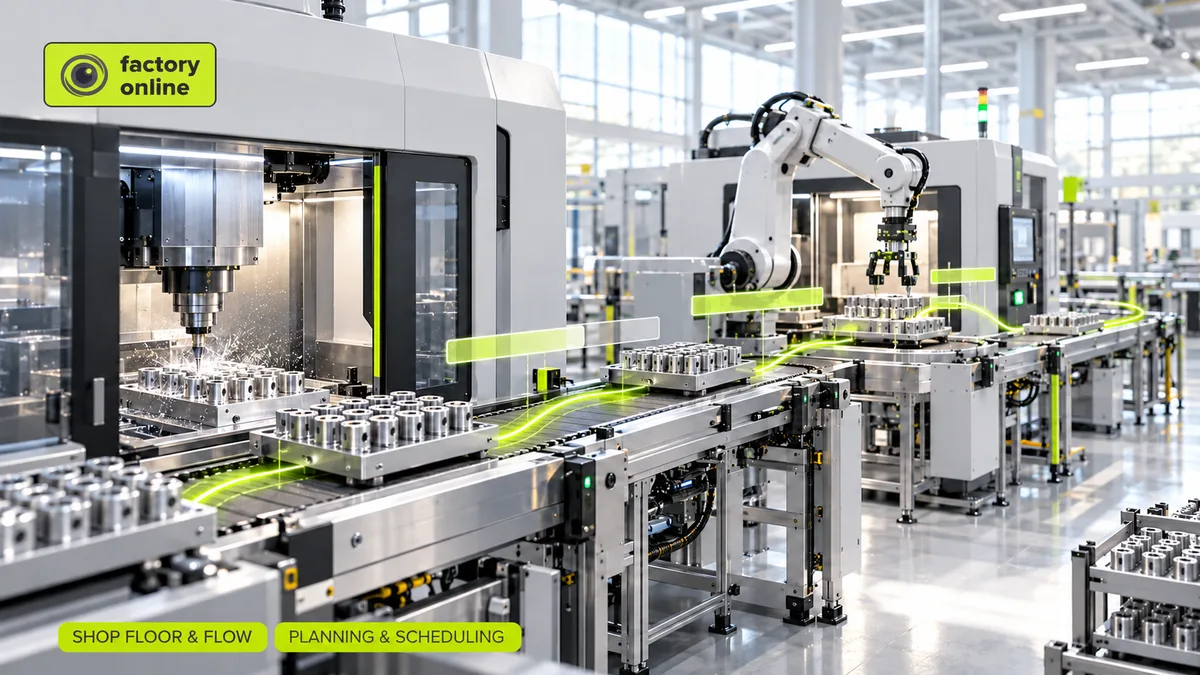
The first machine has completed 100 parts. The next machine is ready, but the route sends work forward only when all 500 are complete.
The second machine waits while usable parts accumulate. The delivery date includes that waiting.
A production batch is the quantity planned for manufacturing. A transfer batch is the quantity moved to the next operation at a time. They can differ where the process and traceability rules permit.
One order can move in smaller groups
A 500-part order might run under one production setup while parts transfer in groups of 100. That does not automatically create five separate production orders or five setups.
Handling, inspection and identification still apply to every transfer. Define when each group becomes eligible for the next operation and how its identity stays connected to the original batch.
Some processes require a complete batch: heat treatment, mixing or batch testing can prevent the overlap assumed in a simple machining example.
A worked example: 16 hours 40 minutes become ten
Assume two different machines, continuous availability and one minute per part at each operation. There is no setup, transport, inspection delay or competing work. The hypothetical order contains 500 parts.
With complete-batch transfer, operation 1 takes 500 minutes. Operation 2 then takes another 500. Total elapsed time is 1,000 minutes, or 16 hours 40 minutes.
With transfer batches of 100, machine 2 starts after the first 100 minutes. The final group leaves machine 1 at minute 500 and finishes machine 2 at minute 600.
Total elapsed time becomes 600 minutes, or 10 hours. The teaching example saves 400 minutes, or 6 hours 40 minutes, through overlap. Processing effort remains 1,000 machine-minutes.
Smaller transfers have a cost
Five transfers instead of one require more handling. If every transfer needs paperwork, inspection or a forklift trip, those costs may offset part of the benefit.
Very small groups can also starve the next operation when the upstream rate is slower or unpredictable. Choose transfer size using the real rates and handling rules.
Check the downstream queue
An overlap helps only if the next resource has a usable slot. Sending 100 parts forward into a three-day queue simply relocates the waiting.
Start with the lead-time breakdown and watch work in progress. Releasing more groups without controlling the queue can make the shop floor harder to manage.
Test the rule on an actual routing
In a factory.online demo, bring one routing where partial transfer is technically permitted. Ask the team to confirm how transfer quantity and overlap can be represented and how the result appears in the schedule.
Book a demo with processing rates and transfer conditions. Compare elapsed time, handling and delivery feasibility rather than assuming the smallest batch is best.
