26 Mar 2026
Inventory Management: The Report Says 500, the Line Is Stopped
The stock report says 500 and the line still stops. Learn the five states of stock, how to calculate turns and days of cover, and how ABC/XYZ sets priorities.
The stock report says 500 housings. The assembly line needs 200 today and stops before lunch for lack of housings. Both statements are true, and every plant manager has lived through a version of this morning.
The gap between them is what inventory management in manufacturing is really about: knowing how much material, work in progress and finished product you have, in what state and where, and keeping just enough of it to run production and ship on time without tying up more cash than you need. Owning 500 is one fact. Being able to use 200 of them at 7 a.m. at line 3 is another.
Inventory management starts with five states of stock
Think of your bank. Your balance may be $50,000, but $30,000 of it sits in a fixed deposit until March. You can't pay a bill with it today. Stock works the same way. Of the 500 housings on the report:
- Available: 120 on the shelf, released, free to use.
- Reserved: 150 already allocated to another order.
- On quality hold: 100 received yesterday, waiting for incoming inspection.
- Somewhere else: 80 in the second warehouse or on a truck between sites.
- Not usable as-is: 50 damaged, expired, the wrong revision or, in cable, remnants too short for any order.
Add them up: 120 + 150 + 100 + 80 + 50 \= 500. The report is correct. The line needs 200 and can use 120. It stops 80 short.
Every one of the five has a different fix. Buying more housings solves none of them. Speeding up inspection solves state 3; a transfer solves state 4; a decision about priorities solves state 2. The waiting-for-inspection problem is covered in raw materials: received isn't usable, and the wrong-place problem in distribution planning.
Raw materials, WIP and finished goods: the map
Manufacturing inventory moves through three stages, and each hides stock in its own way.
- Raw materials and purchased parts. Arrive, get inspected, get stored, get issued. The risks: stock received but not released, and stock booked in the wrong location.
- Work in progress (WIP). Everything issued to production and not yet finished, including semi-finished items that sit between operations. The risk: nobody knows exactly where it is or how old it is. Some plants give subassemblies their own item numbers so they can be stocked and counted, a choice explained in semi-finished goods. Too much WIP also stretches lead time, which is Little's Law at work.
- Finished goods. Made, but not always shippable: waiting for final inspection, packing or paperwork. That gap is the subject of finished goods: finished, but can't ship.
Inventory turns and days of cover, worked
Two numbers tell you whether you carry too much or too little.
Inventory turns look backward: how many times a year your average inventory is used up.
Say your annual cost of goods sold is $6,000,000 and average inventory is $1,500,000. Turns \= 6,000,000 ÷ 1,500,000 \= 4. On average, stock sits for 365 ÷ 4 \= about 91 days before it is used.
Cut average inventory to $1,000,000 at the same sales and turns rise to 6, about 61 days. That frees $500,000 of cash. If carrying stock costs you around 20% a year (capital, space, insurance, obsolescence), that is roughly $100,000 a year saved.
Days of cover look forward: how long current stock will last at expected usage. It works best per item.
You hold 3,000 m of a copper conductor and use 150 m a day. Days of cover \= 3,000 ÷ 150 \= 20 days. If the supplier's lead time is 30 days, you are already late to reorder, even though 3,000 m looks like a lot. Setting that reorder point properly is covered in safety stock and reorder point.
Use days of cover on available stock, not on the total. For the housings above, 500 on hand at 200 a day looks like 2.5 days of cover. Usable, it is 120 ÷ 200 \= 0.6 days: the line stops before lunch.
ABC/XYZ: not every item deserves the same attention
A plant with 5,000 items can't watch all of them daily. ABC/XYZ sorts them in two directions.
ABC by value: A items are the few that make up most of your annual consumption value (typically about 80% of the value from about 20% of the items); C items are the long tail of cheap parts.
XYZ by predictability: X items are used steadily, Y items fluctuate, Z items are used rarely and irregularly.
| X (steady) | Y (fluctuating) | Z (sporadic) | |
|---|---|---|---|
| A (high value) | Plan tightly from MRP, low buffer | Plan from MRP, review weekly | Buy or make to order only |
| B (medium) | Reorder point | Reorder point with safety stock | Make to order, small buffer |
| C (low value) | Generous stock, two-bin | Generous stock | Keep a few or buy on demand |
The logic: spend planner attention where money and uncertainty meet (AY, AZ), and let cheap, steady items look after themselves.
Myth: more stock means fewer shortages
It is the most natural belief in operations and often the opposite of true. More stock means more places for it to hide, more of it in the wrong state, and more cash that can't buy the part you actually lack. Plants with bloated warehouses often have the most shortages, because the money went into the wrong items. The fix is better-shaped stock: the right items, in the right state, in the right place.
FAQ
What is a good inventory turn rate for a manufacturer? It depends heavily on the industry and on make-to-order versus make-to-stock. Compare against your own trend and similar plants rather than a universal number.
Should WIP count as inventory? Yes. It is money already spent on material and labor, and it sits on the balance sheet like any other stock.
How it looks in factory.online
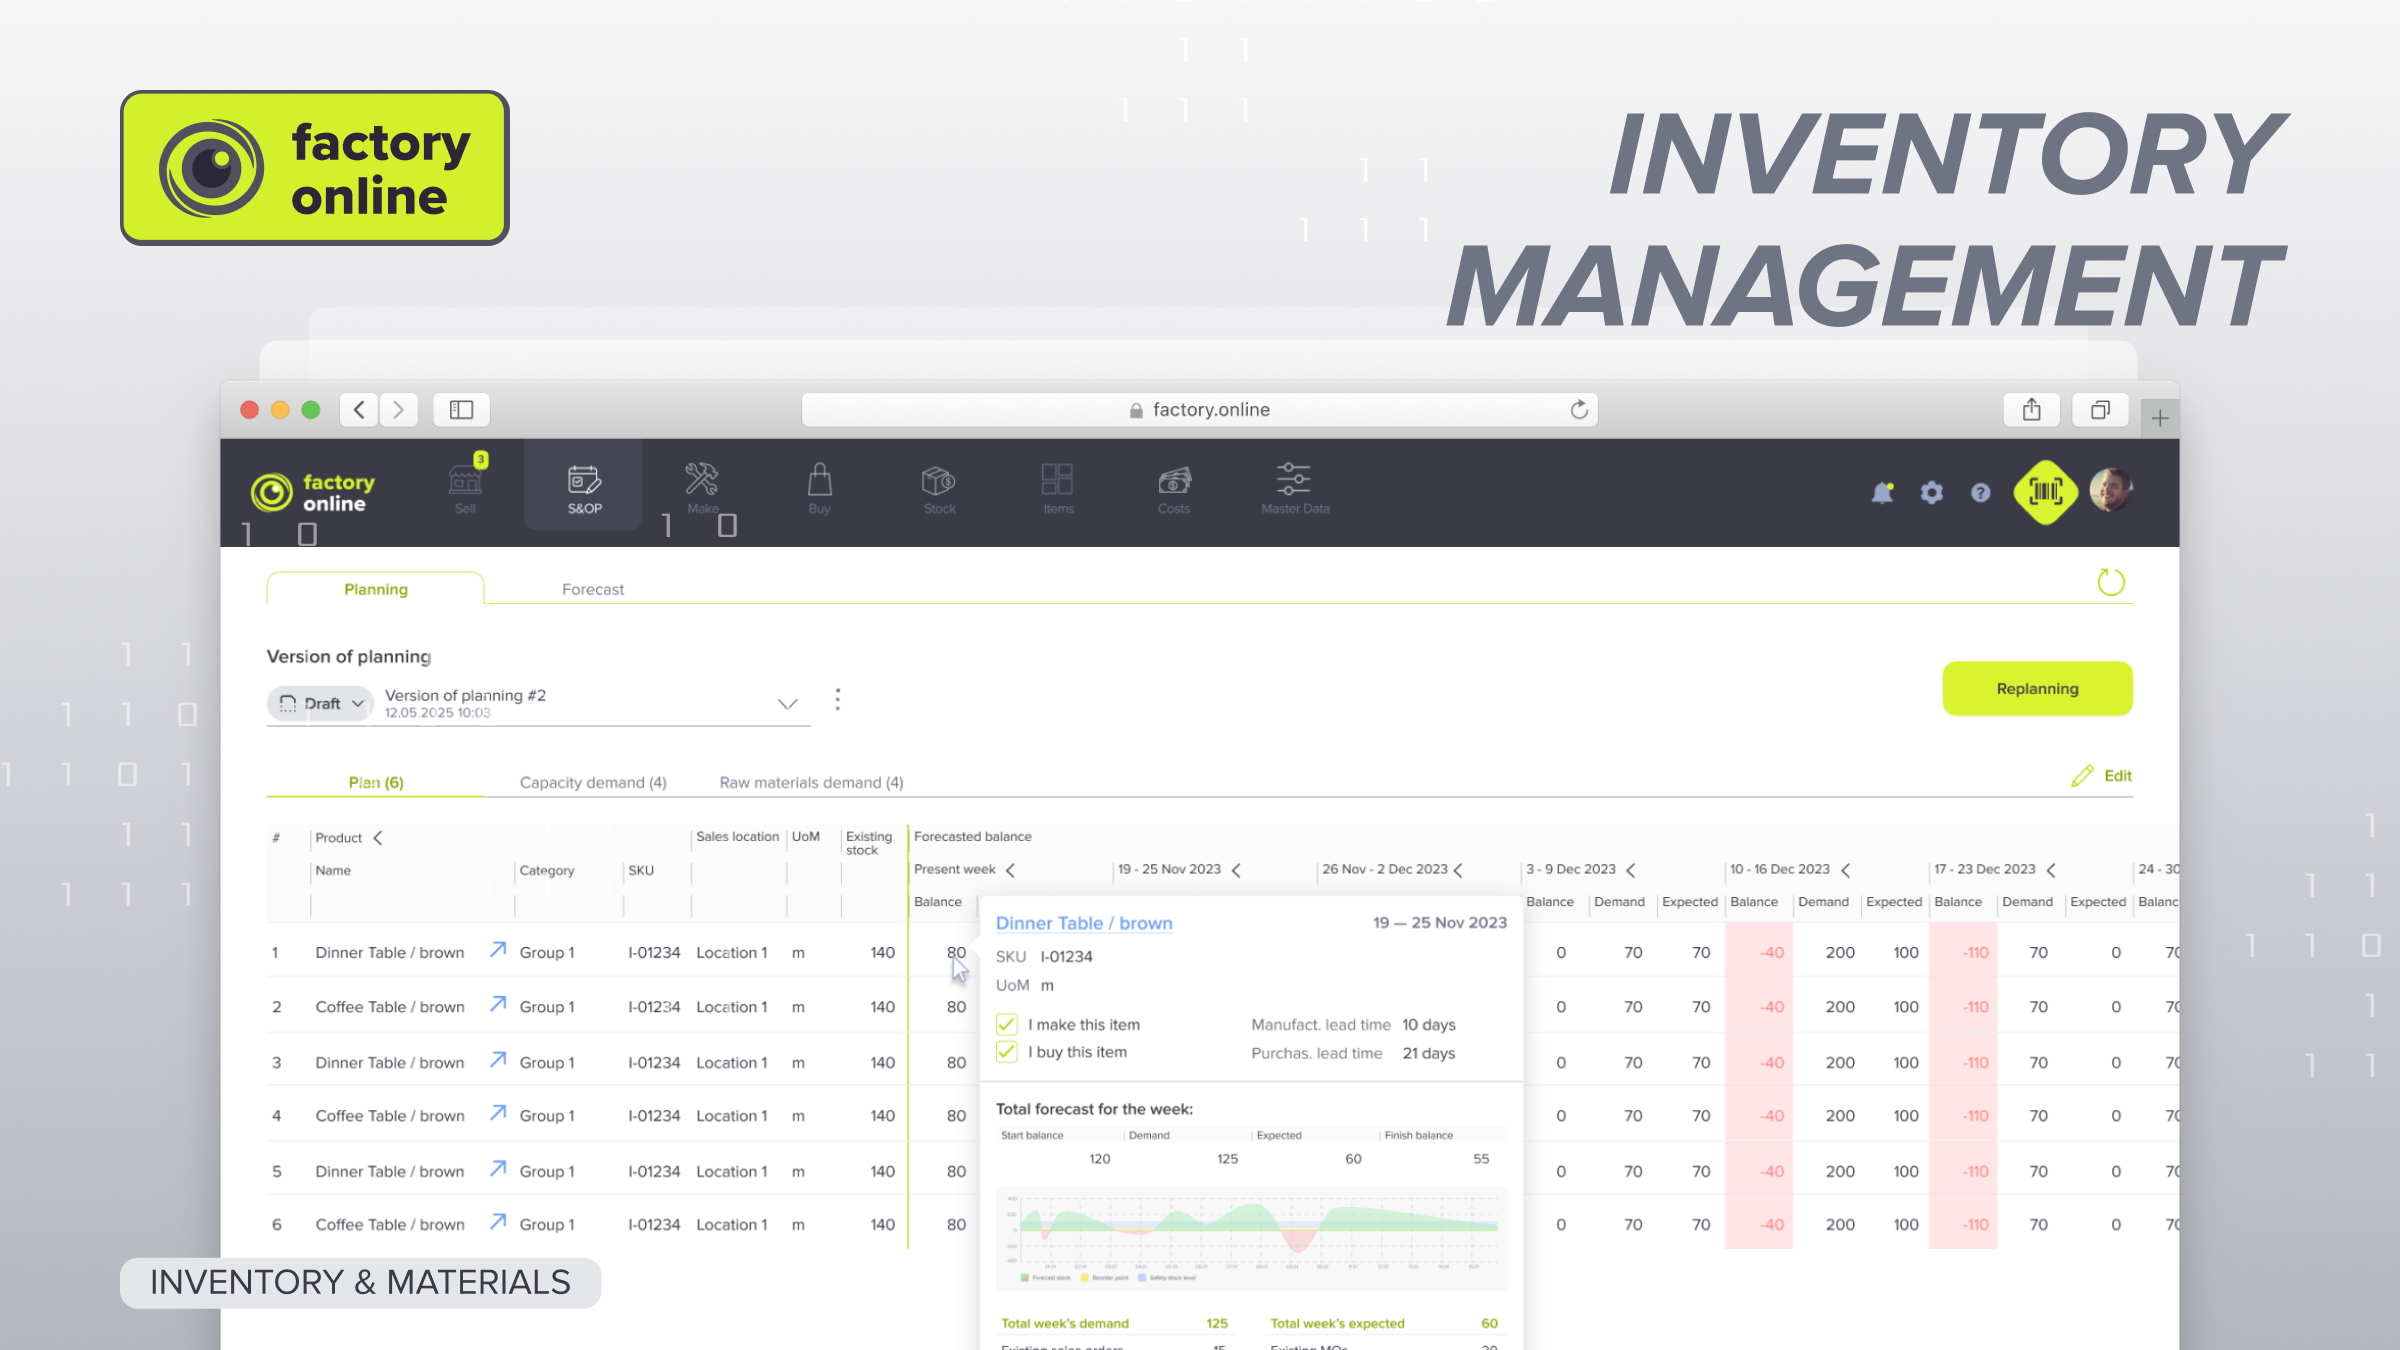
In factory.online, stock is kept per location and per batch, with quality holds visible, so the planner sees the 500 housings split into their real states instead of one total. MRP works from stock, open supply and multi-level BOMs and links each shortage to the order it would stop. For cable and wire, batches and containers carry their own lengths, so a remnant shows as 40 m, not as part of a total.
If your stock report and your line keep disagreeing, book a demo and bring the report.