5 Jan 2026
Why ERP Thinks Every Order Takes 10 Days (Your Factory Disagrees)
Three Friday orders, one furnace, a half-shift changeover. See why ERP production planning uses fixed lead times, how sequence decides who is late, and when ERP scheduling is enough.
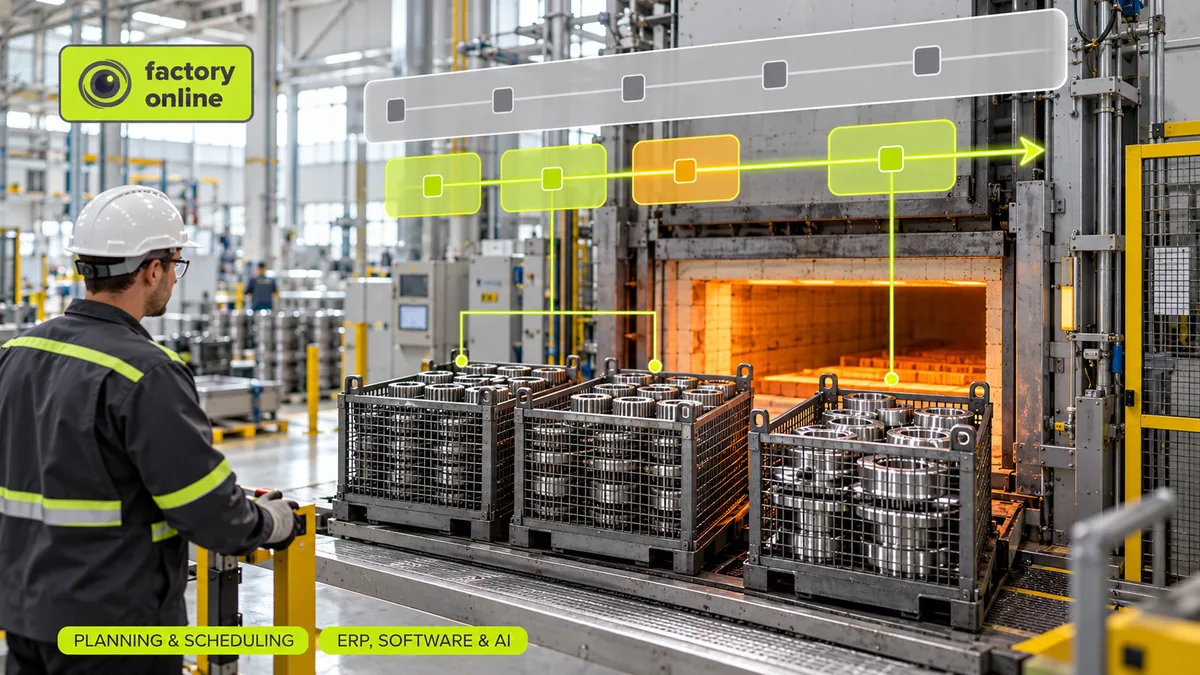
Three orders are due Friday. All three need the same furnace. Two use the same steel grade, one uses a different grade, and switching grades takes half a shift. Your ERP says all three are fine: each was released with its standard 10-day lead time, and the furnace shows only 83% load. The furnace operator already knows one of them will be late. Who's right?
Both, in their own way. ERP production planning is the planning your ERP system does out of the box: it takes sales orders and stock, calculates material needs with MRP, and sets production dates using fixed lead times. What it usually does not do is check whether the machines can actually run the work in that time, in that order. That gap is where most "why is this late?" conversations start.
Why ERP uses fixed lead times
ERP planning grew out of MRP, which was built in the 1960s to answer one question: which materials, how many, and when. To make that arithmetic possible on the computers of the day, it made a bold simplification. Every item gets a lead time, a fixed number of days, and the plan counts backward from the due date.
That simplification is still there. If a welded frame has a 10-day lead time, the ERP assumes 10 days whether the welding cell is empty or has three weeks of backlog. In other words, it assumes infinite capacity. The full history of how capacity was bolted on later, and what MRP II and APS added, is told in MRP vs MRP II vs ERP vs APS.
Think of a GPS that always says "20 minutes to the office", at 3 a.m. and in rush hour alike. The number is an average. It's right on some days and badly wrong on the days that matter.
The myth: "Our lead times are wrong, let's fix them"
When orders keep finishing late, the first reaction is to raise the lead times. Make it 12 days, then 14. It rarely helps, because the problem isn't the number. It's that the number is fixed while real lead time depends on the load.
Say the furnace has 2 days of queued work. A new order waits 2 days, runs, and moves on. Next month the queue is 8 days. The same order now waits 8 days. No single fixed value can be right in both months.
Worse, longer lead times make orders get released earlier, which puts more work in the queue, which makes real lead times longer. Planners call this the lead-time spiral. Where the time actually goes, mostly waiting, is explained in manufacturing lead time.
Worked example: A→B→C vs A→C→B
Back to the furnace. It runs around the clock and is already set up for grade X. The three orders can start Thursday 06:00 and must be out by Friday 18:00. That's a 36-hour window.
- Order A: grade X, 12 hours
- Order B: grade Y, 10 hours
- Order C: grade X, 8 hours
- Changeover between grades: 4 hours (half a shift)
Total run time is 12 + 10 + 8 = 30 hours. In a 36-hour window that's 30 / 36 = 83% load. The ERP's rough capacity view is happy.
Sequence A → B → C (the order they were entered):
- A: Thursday 06:00–18:00
- Changeover X→Y: 18:00–22:00
- B: Thursday 22:00–Friday 08:00
- Changeover Y→X: 08:00–12:00
- C: Friday 12:00–20:00
Total 12 + 4 + 10 + 4 + 8 = 38 hours. Order C finishes 2 hours late.
Sequence A → C → B:
- A: Thursday 06:00–18:00
- C: Thursday 18:00–Friday 02:00 (same grade, no changeover)
- Changeover X→Y: 02:00–06:00
- B: Friday 06:00–16:00
Total 12 + 8 + 4 + 10 = 34 hours. Everything is done by 16:00, with 2 hours to spare.
Same orders, same furnace, same hours of work. The only difference is sequence, and the ERP never saw it. Its lead-time math said "fine" for both. Its load view said 83% for both. Only a schedule that knows the changeover rule can tell them apart.
What ERP production planning does well
This is not an anti-ERP story. ERP is the right system for a lot of planning work:
- Orders, stock and money. Sales orders, purchase orders, goods receipts, inventory valuation and costing belong in the ERP.
- Material requirements. MRP explosion through the BOM is exactly what it was built for.
- Stable, simple flows. A paced line making a narrow range, with spare capacity and few changeovers, may never need anything more.
Some ERP suites also offer detailed-scheduling add-ons. If yours has one, it's configured, and planners actually use it, you may be covered.
When ERP scheduling is not enough
You probably need a finite-capacity planning layer if several of these sound familiar:
- Orders compete for a few shared machines, like a furnace, an extruder or a paint line.
- Changeover times depend on sequence, so "what came before" matters.
- The planner rebuilds the real schedule in Excel every morning. Seven signs the spreadsheet has stopped working is a quick self-test.
- Sales promises dates from the ERP, and production quietly moves them.
- A breakdown on Tuesday takes a day to replan by hand.
The usual answer is not to replace the ERP. It's to let the ERP keep doing orders, stock and finance, and to add a planning tool that does capacity and sequence. That raises its own question: which system owns which data, and how do they stay in sync? That's the subject of ERP integration for production planning. For the broader path from spreadsheet to scheduling tool, see manufacturing planning software.
How factory.online helps
factory.online runs alongside an ERP, with integrations for SAP and Microsoft Dynamics 365. In the furnace example, the planner sees orders A, B and C on a finite-capacity Gantt, with grade changeovers as real blocks of time, and sees order C turn late when B is slotted between two grade-X jobs. The planner can move C ahead of B, recalculate, and compare both sequences in a planning scenario before touching the live plan. MRP and rough-cut capacity checks run on the same data, so the material plan and the machine plan don't drift apart.
FAQ
Is APS a replacement for ERP? No. APS (advanced planning and scheduling) handles capacity and sequence. ERP remains the system of record for orders, stock and finance. They work together.
Can I just use infinite-capacity planning with a buffer? For stable flows, often yes. When changeovers depend on sequence or a few machines are shared, a buffer hides the problem until the week it doesn't.
Why does ERP show 83% load and still miss the date? Because load counts hours, not order. Changeovers, sequence and timing within the window decide whether the work fits.
If your ERP says "fine" and your furnace operator says "late", book a demo and bring that Friday with you.